Surface Preparation Standards — SA1, SA2, SA2.5 & SA3 Explained
Surface Preparation Standards — SA1, SA2, SA2.5 & SA3 Explained is rarely just about making steel look cleaner. On sites across North West England, it is usually part of a wider maintenance, coating or refurbishment decision where the client needs a predictable surface condition, realistic programme control and a contractor who understands how blasting affects the next trade. Early planning with surface preparation and steel pre-treatment in North West England often helps define the correct work fronts, the safest access plan and the point at which blasting stops being a cleaning activity and becomes a technical surface-preparation process.
That distinction matters commercially. If the specification is vague, a project can look cheaper on paper but still lose time once the coating inspector, maintenance team or shutdown planner asks for a finish the original scope never properly defined. A survey-led approach gives buyers in North West England a more defensible programme, clearer cost assumptions and a better handover standard.
Why this topic matters on real industrial sites
In practice, the key issue is understanding how blast-cleaning standards affect coating performance, steel cleanliness and inspection expectations. That means the contractor is not just removing visible contamination; they are working toward an outcome that supports coating adhesion, corrosion control, inspection quality or safer access. On live industrial sites, those outcomes depend on method choice, access constraints, environmental controls and how well the work is sequenced with everyone else using the same space.
A realistic specification also needs to reflect the substrate and operating environment. North West projects that involve bridges, marine assets and exposed structural steel often need a clearly stated preparation grade to avoid disputes about finish quality later. When those site conditions are ignored, teams often end up reworking steel, extending access hire or delaying the follow-on coating crew while the blast scope is clarified mid-project.
What a realistic shot-blasting scope usually includes
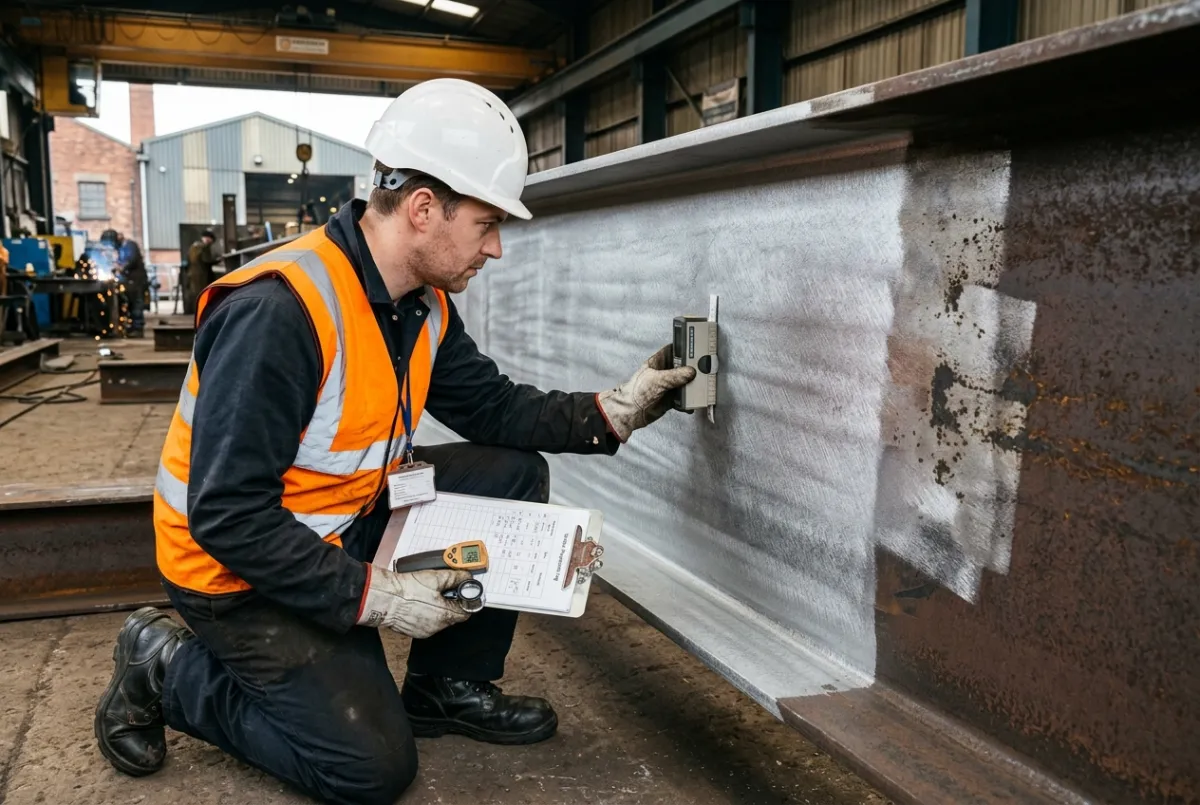
A credible scope often covers the recognised preparation grades used to describe how thoroughly rust, mill scale, coatings and contamination have been removed before coating application. Good contractors define what will be prepared, which areas need protection, what standard is required, how debris will be managed and how the cleaned surface will be checked before handover. That is an important E-E-A-T signal on blasting work because it shows the contractor understands the difference between a dramatic visual change and a technically usable finish.
| Work option | Best fit | Typical duration or cost band | Expected outcome |
|---|---|---|---|
| SA1 | Light blast cleaning | Looser contamination removal | Lower-spec maintenance situations |
| SA2 | Thorough blast cleaning | Better removal of mill scale and rust | General industrial preparation |
| SA2.5 | Very thorough blast cleaning | Commonly specified for durable coatings | Marine, bridge and exposed steel systems |
| SA3 | Blast-clean to visually clean steel | Highest visual standard | Critical or premium coating systems |
Costs, timing and planning assumptions
Selecting a higher preparation standard can increase labour and abrasive consumption, but it often reduces coating risk where durability and inspection performance matter most. For buyers comparing approaches, HSE surface engineering guidance is a useful reference because it reinforces that blasting work must be supported by competent equipment selection, exposure control and safe operating practice rather than treated like a simple washdown.
What usually changes the programme or budget
The biggest variables are normally access method, containment, coating condition, steel complexity, inspection hold points, waste handling and how quickly the next trade needs the surface released. On larger North West projects, programme length is often shaped just as much by logistics and handover sequencing as by the blast rate itself.
Local delivery considerations
The strongest specifications link the SA standard to the coating system, exposure environment, inspection hold points and the time allowed before priming begins. Teams looking at related project examples elsewhere in the network often find high-level surface preparation in North West and North Wales useful because it shows how comparable industrial environments deal with access, contamination, sequencing and handback expectations. That wider context helps procurement teams set realistic expectations before the project starts.
Local knowledge also matters commercially. Haulage restrictions, wind exposure, shared estates, port traffic, older structures and short maintenance windows all influence how abrasive blasting is phased and how quickly cleaned steel can move to the next stage. Those details do not always appear in a headline quote, but they often decide whether a project runs smoothly.
How experienced contractors reduce disruption
Experienced contractors reduce disruption by agreeing the release order early, mapping exclusions, checking equipment before mobilisation and treating inspection points as part of the project rather than an afterthought. The strongest specifications link the SA standard to the coating system, exposure environment, inspection hold points and the time allowed before priming begins. On many jobs, the finished result is better when the blasting scope is planned alongside industrial and protective coatings in North West England because coating performance, access planning and steel condition rarely sit in isolation on a busy industrial site.
Frequently asked questions
Why do SA standards matter?
They give the client, contractor and coating inspector a shared reference for how thoroughly the surface should be cleaned before paint is applied.
Is SA2.5 common on coating projects?
Yes. SA2.5 is widely specified where a very thorough blast clean is needed for durable coating performance on exposed steel.
Does a higher SA grade always mean a better project?
Only if it matches the coating system, substrate condition and service environment. The preparation grade should follow the specification, not guesswork.
Request a shot-blasting project quote
If you need support with surface preparation standards SA1 SA2 SA2.5 and SA3 in North West England, request a project survey and quote from Alternative Cleaning Solutions (NW) Ltd. We will review the substrate, explain the safest preparation route and build a practical programme around access, containment, coating requirements and site downtime.